

A structural fabrication plant can have enough steel, skilled workers, and machine capacity yet still struggle to answer a basic question: which members will actually be ready for the next dispatch?
That gap is rarely caused by one isolated machine. It develops when drawings, mark numbers, materials, jobcards, process updates, quality decisions, and dispatch priorities are managed separately.
Modern structural steel shopfloor management connects these moving parts around the actual fabrication route, giving teams one view of what must be made, what is blocked, and what is ready.
This does not mean forcing every fabricator into the same sequence. A beam, plate assembly, and subcontracted job may follow different processes. The control system must follow the route defined for the job.
Where Structural Fabrication Shops Usually Lose Control
Structural fabrication is project-driven. One project can contain thousands of similar-looking parts that differ in dimensions, hole patterns, material grade, revision, or destination.
As workload grows, teams often create separate trackers for drawings, cutting, fabrication, inspection, painting, and dispatch. The production meeting may rely on yesterday’s spreadsheet, while the shopfloor has already moved some members forward and held others for rework.
Supervisors then spend time calling departments and walking through the plant to establish the real status.
These are among the common manufacturing challenges in fabrication. Information exists, but it is fragmented, delayed, and difficult to connect to the physical steel member.
Start With a Reliable Project and Production Structure
Shopfloor control begins before cutting starts. The system needs a clear hierarchy that reflects how the business plans and executes work.
Depending on the fabricator, this structure may include:
- Customer
- Project
- Structure
- Assembly
- Mark number
- Piece quantity
- Dispatch lot
Management needs project-level progress and delivery risk, while production needs a precise list of members, quantities, drawings, material requirements, and routes.
Work orders should therefore be released against approved requirements with a defined scope, priority, route, and required date.
Build Control Around the Fabrication Identity
The mark number is the operational identity of a fabricated component or assembly. It connects the physical member with the information needed to manufacture, inspect, move, and dispatch it.
A practical guide to mark numbers in structural steel fabrication explains this foundation in more detail.
Good control requires more than storing the mark in a master list. The shopfloor must be able to identify:
- The applicable drawing and revision
- Material grade, section, or plate specification
- Required quantity and completed quantity
- Configured fabrication route
- Current process and physical location
- Inspection, hold, and rework status
- Project, assembly, and dispatch linkage
A barcode or QR code can make this connection faster, but the code itself does not create traceability. It must open a valid digital record and capture meaningful transactions as the member moves through production.
Keep Drawings and Revisions Connected to Execution
Revision control becomes dangerous when updated drawings circulate through email or messaging groups while old prints remain on the shopfloor.
A worker may fabricate correctly according to the document in hand and still produce the wrong component.
A controlled workflow should show which drawing revision is approved for production. When engineering issues a change, the team should be able to identify the affected marks and their current production status.
Material that has not yet been processed may simply follow the revised drawing. Work already cut, fabricated, or inspected may require a specific review and decision.
The objective is to ensure that production does not proceed without clear, current, and accessible information.
Connect Material Availability With Production Release
Steel availability cannot be treated as a simple yes-or-no stock check. The required section, plate thickness, material grade, heat or batch, usable length, and reservation status may all affect whether work can start.
Consider a planner who sees sufficient plate quantity in a spreadsheet and releases ten marks. On the shopfloor, part of that stock is reserved for another urgent project, while another plate is waiting for inward inspection.
The released work now joins the production queue but cannot be completed. This creates avoidable WIP and repeated rescheduling.
Material should be checked and allocated against actual production requirements. For plates and sheets, this includes visibility into:
- Usable stock
- Available dimensions
- Reserved material
- Remnants
- Material issue history
- Material waiting for inspection
The principles covered in material management of sheets are especially relevant where nesting and remnant use influence both material availability and cost.
Use Configurable Routes, Not One Universal Process Flow
Structural fabrication plants rarely have one route that applies to every job. Processes can vary by product type, customer specification, material, surface-treatment requirement, and available equipment.
A digital system should allow the relevant route to be configured for an item, mark, assembly, or production order.

For example:
- Route A: Cutting → Drilling → Fit-up → Welding → Inspection → Painting
- Route B: Cutting → Punching → Bending → Inspection → Dispatch
- Route C: Cutting → Fabrication → Subcontract Galvanizing → Final Inspection
These are example routes, not a universal sequence.
Route-based control tells each work centre what is ready, what must happen next, and which previous operation must be accepted before work proceeds.
It also prevents a project-level completion percentage from hiding delays at one critical fabrication stage.
Replace Paper Jobcards With Point-of-Work Updates
Paper jobcards are useful for carrying instructions, but they become weak reporting tools when entries are collected and entered hours or days later.
By then, planning and production teams are working with an outdated view.
A digital jobcard can carry:
- Mark number
- Drawing reference
- Planned quantity
- Configured route
- Current operation
- Work centre
- Inspection requirements
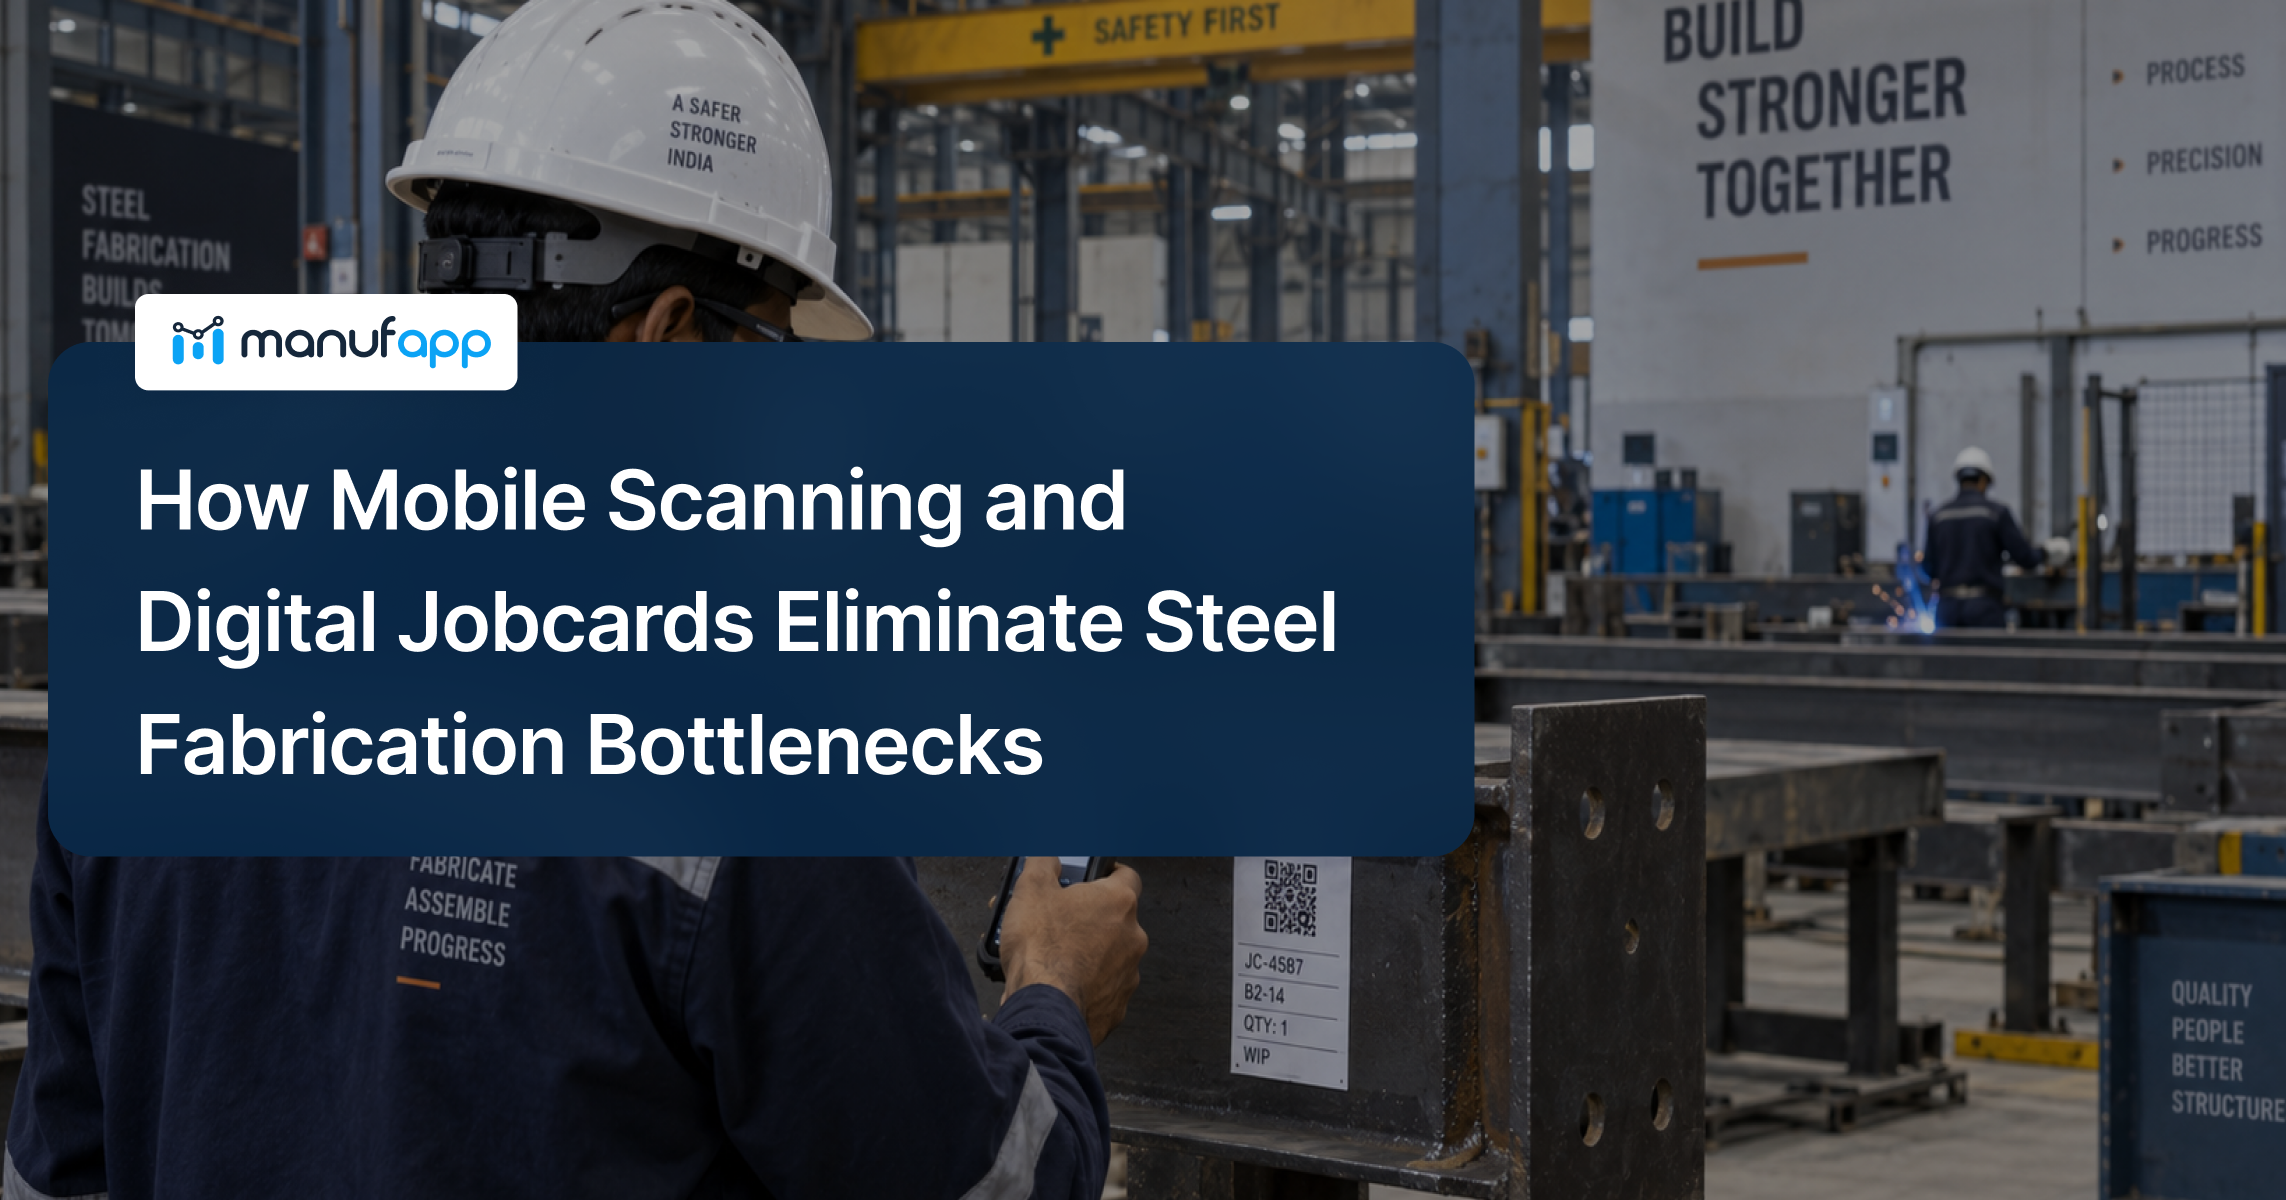
A QR code or barcode lets an operator open the correct production task on a mobile device or workstation.
At each reporting point, the user should record the accepted quantity, rejected quantity, production status, time, work centre, and any hold or issue.
This is the practical value of barcode-based production entry: it reduces the time between the physical production event and the system update.
ManufApp supports configurable jobcards and scan-based shopfloor reporting, allowing the digital workflow to reflect the fabricator’s actual processes instead of imposing one fixed route.
Make WIP and Bottlenecks Visible by Process
Total production completed does not tell a plant manager where delivery risk is building.
Teams need to see how many marks or quantities are waiting at each stage, how long they have been there, and why they have not moved.
Useful WIP views may show:
- Marks waiting to start at a work centre
- Work completed at one process but not received at the next
- Quantities held for inspection
- Members sent for rework
- Operations exceeding planned completion dates
- Subcontracted work awaiting return
- Dispatch-critical members still incomplete
This is where many factories lose output despite having a production plan.
The wider issue of why output gets lost between planning and dispatch applies directly to structural fabrication. Execution constraints often remain hidden until they threaten a committed dispatch date.
A useful dashboard should lead to action. If welding WIP is rising, the team should be able to identify the affected marks, dates, projects, and reasons instead of seeing only a red indicator.
Treat Quality Holds and Rework as Part of the Route
Quality inspection cannot sit outside production tracking.
If a member is rejected or held but still appears as completed, every downstream production and dispatch number becomes unreliable.
Inspection requirements may differ by project and process. These can include:
- Dimensional inspection after fit-up
- Weld inspection
- Surface inspection
- Painting or coating checks
- Final inspection before dispatch
The inspection result should remain connected to the relevant mark or assembly, along with the observation, disposition, and approval.
When rework is required, the system should return the affected quantity to a defined operation or rework stage.
Production should see that the member is not ready for the next process. Planning should also see the possible effect on the production and dispatch schedule.
This creates a clear audit trail without treating rework as an informal activity outside the production plan.
Manage Subcontracting Without Losing Visibility
Activities such as galvanizing, machining, testing, or specialized coating may take place outside the factory.
Teams must track:
- Which marks were sent
- Quantity sent
- Subcontractor details
- Dispatch date
- Expected return date
- Received quantity
- Rejected quantity
- Shortages
- Pending balance
Returned work must rejoin the correct production route and inspection workflow.
Without this connection, the internal dashboard may show a project as nearly complete even though a dispatch-critical batch is still with the subcontractor.
Link Production Progress to Dispatch Readiness
A member is not dispatch-ready merely because fabrication is complete.
It may still require final inspection, painting, identification, documentation, packing, or grouping with other members required at the project site.
Dispatch planning should therefore work from a readiness check rather than a manually reported completion percentage.
The dispatch team should be able to group eligible items according to:
- Project
- Structure or assembly
- Erection sequence
- Customer priority
- Vehicle plan
- Delivery schedule
The system should also show the exact pending reason for every member excluded from the dispatch plan.
This becomes especially important when a project has partial dispatches. Loading whatever is visible in the yard may improve short-term dispatch tonnage but create erection problems if connected members or assemblies are missing.
What Good Structural Steel Shopfloor Management Looks Like
Good control is visible in daily decisions, not in the number of reports available.
Planning releases work that has the required information and material. Operators know the next task and the correct drawing revision. Quality holds prevent premature movement. Managers can see where WIP is accumulating. Dispatch works from confirmed readiness.
The system should answer five questions quickly:
- What must be produced next, and why?
- Is the required material and approved information available?
- Where is each mark or assembly now?
- What is blocked, delayed, rejected, or under rework?
- Which items are genuinely ready for dispatch?
ManufApp brings production orders, configurable process routes, digital jobcards, scan-based reporting, quality status, and dashboards into a connected execution flow.
The objective is not to digitise every existing register. It is to create timely and reliable control from production release through dispatch.
A Practical Rollout Sequence
Trying to digitise the entire fabrication plant in one step can reproduce existing confusion inside a new system.
A phased rollout keeps the scope measurable.
Start with one project, product family, or fabrication area. Clean the essential masters, define the production hierarchy, and validate the mark-level data.
Next, configure the actual fabrication routes and establish jobcard and reporting points. Quality decisions and dispatch readiness can then be connected to the same execution flow.
Once users trust the production status shown in the system, the workflow can be expanded to additional processes, projects, and integrations.
Dashboards should come after transaction discipline. Otherwise, they simply visualise incomplete or unreliable data.
Frequently Asked Questions
Is one standard process route suitable for every structural fabricator?
No. Routes vary according to the product, project, customer requirements, and plant capabilities. The system should support configurable routes and track each job against the process sequence that actually applies.
Are QR codes necessary for fabrication tracking?
QR codes are useful for fast identification and production reporting, but they are not the complete solution.
Reliable masters, controlled jobcards, meaningful production updates, and quality status are equally important.
Should fabrication progress be tracked by weight, quantity, or mark number?
Most structural fabrication plants need more than one measure.
Quantity and mark status support shopfloor execution and traceability, while weight can support project-level progress and dispatch planning. The selected metric must not hide incomplete, dispatch-critical members.
How does digital shopfloor management reduce fabrication WIP?
It exposes where work is waiting, why it is blocked, and which downstream operation is constrained.
Teams can then release work more selectively and resolve the cause of accumulation instead of continuously adding new jobs to the shopfloor.
What should a structural fabrication company digitise first?
Begin with the production structure, mark identification, approved drawings, material availability, fabrication routes, and a small number of reliable reporting points.
Strong structural steel shopfloor management grows from accurate shopfloor transactions, not from adding dashboards first.